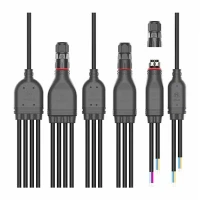
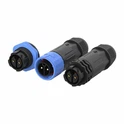
As a supplier of A16 waterproof connectors, I often receive inquiries from clients in various industries, including the food - processing sector. The question "Can the A16 waterproof connector be used in food - processing equipment?" is one that comes up quite frequently. In this blog post, I'll delve into this topic, considering the technical specifications of the A16 waterproof connector and the requirements of food - processing equipment.
Technical Features of A16 Waterproof Connectors
First, let's understand the characteristics of A16 waterproof connectors. These connectors are designed with high - quality materials and advanced manufacturing techniques. The connectors are engineered to provide reliable electrical connections even in harsh environments, which is a crucial factor when considering their use in food - processing equipment.
The A16 waterproof connectors come in different pin configurations, such as the A16 3pin Waterproof Connector, A16 5pin Waterproof Connector, and A16 2+4pin Waterproof Connector. Each configuration is tailored to meet specific electrical connection needs.
One of the key features of A16 waterproof connectors is their excellent waterproof performance. They are rated to withstand immersion in water to a certain depth for a specified period, which is essential in food - processing environments where equipment is often washed down with water or exposed to high - humidity conditions. The connectors are also resistant to dust and other contaminants, ensuring that the electrical connections remain stable and reliable over time.


Requirements of Food - Processing Equipment
Food - processing equipment has strict requirements in terms of safety, hygiene, and reliability. From a safety perspective, all electrical components used in food - processing equipment must meet relevant electrical safety standards to prevent electrical hazards such as short - circuits and electric shocks.
Hygiene is another critical aspect. The equipment must be easy to clean and disinfect to prevent the growth of bacteria and other microorganisms. Any materials used in the equipment, including connectors, should be non - toxic and resistant to the chemicals commonly used in food - processing cleaning and disinfection procedures.
Reliability is also of utmost importance. Food - processing operations are often continuous, and any downtime due to equipment failure can result in significant losses. Therefore, the connectors used in the equipment must be able to withstand the mechanical stresses, temperature variations, and electrical loads associated with food - processing operations.
Compatibility of A16 Waterproof Connectors with Food - Processing Equipment
When it comes to safety, our A16 waterproof connectors are designed and tested to meet international electrical safety standards. They are equipped with proper insulation and grounding mechanisms to ensure that they can be safely used in food - processing equipment.
In terms of hygiene, the materials used in the A16 waterproof connectors are carefully selected. They are non - toxic and resistant to common cleaning agents used in the food - processing industry. The smooth surface of the connectors makes them easy to clean, reducing the risk of bacteria accumulation.
Regarding reliability, the A16 waterproof connectors are built to last. Their robust construction can withstand the mechanical vibrations and shocks that are common in food - processing equipment. The waterproof and dust - proof design ensures that the connectors can maintain stable electrical connections even in the harsh environments of food - processing plants.
Case Studies
To further illustrate the suitability of A16 waterproof connectors in food - processing equipment, let's look at some real - world examples. A large - scale bakery was experiencing frequent electrical connection problems with their dough - mixing machines. The previous connectors were not waterproof, and the high - humidity environment in the bakery was causing corrosion and short - circuits. After replacing the connectors with our A16 waterproof connectors, the electrical connection problems were eliminated. The bakery was able to operate their dough - mixing machines continuously without any electrical - related downtime.
Another example is a meat - processing plant. They were using equipment that required frequent washdowns. The old connectors were not able to withstand the water and chemical exposure, leading to frequent failures. After switching to our A16 waterproof connectors, the reliability of the equipment improved significantly. The connectors were able to maintain a stable electrical connection even after repeated washdowns.
Potential Challenges and Solutions
While A16 waterproof connectors are well - suited for food - processing equipment, there are still some potential challenges that need to be considered. One challenge is the compatibility with different types of food - processing equipment. Some specialized equipment may have unique electrical requirements or physical constraints.
To address this challenge, our technical support team is always ready to work with clients to customize the connectors to meet their specific needs. We can adjust the pin configuration, cable length, and other parameters to ensure that the connectors fit perfectly with the equipment.
Another potential challenge is the long - term effects of chemical exposure. Although the A16 waterproof connectors are resistant to common cleaning agents, some specialized chemicals used in certain food - processing operations may pose a threat. In such cases, we can provide connectors with additional protective coatings or use alternative materials that are more resistant to these chemicals.
Conclusion
In conclusion, the A16 waterproof connectors can indeed be used in food - processing equipment. Their excellent waterproof, dust - proof, and chemical - resistant properties, combined with their compliance with safety standards and reliability, make them a suitable choice for this industry.
If you are in the food - processing industry and are looking for high - quality waterproof connectors for your equipment, we invite you to contact us for a detailed discussion. Our team of experts can help you select the right connectors for your specific needs and provide you with the best solutions. We are committed to providing our clients with the highest level of service and the most reliable products.
References
- International Electrotechnical Commission (IEC) standards for electrical safety in industrial equipment.
- Food and Drug Administration (FDA) guidelines for materials used in food - processing equipment.
- Industry reports on the requirements of food - processing equipment.